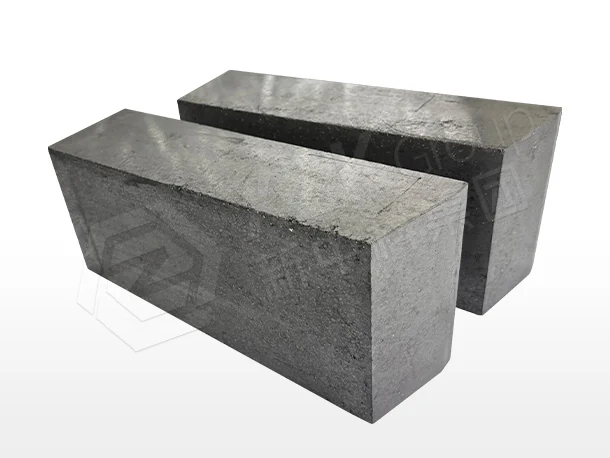
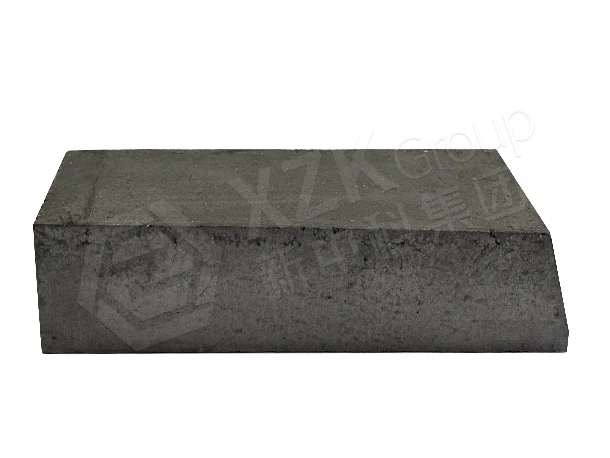
ASC Brick (Al₂O₃-SiC-C) for Torpedo Cars & Hot Metal Ladles
Al₂O₃ ≥53–62% · SiC ≥11.5–14% · C ≥5–11.5% · BD ≥2.75–2.90 g/cm³ · AP ≤8.5–11% · CCS ≥40–50 MPa — torpedo car working lining standard.
Specifications of XZK ASC Brick (Al₂O₃-SiC-C)
Manufactured strictly in accordance with ASTM, ISO, and YB/T metallurgical refractory standards.
| Property | XZK-ASC-A | XZK-ASC-B | XZK-ASC-Mortar |
|---|---|---|---|
| Type | Al₂O₃-SiC-C brick | Al₂O₃-SiC-C brick | Al₂O₃-SiC-C mortar |
| Al₂O₃ (%) ≥ | 53.0 | 62.0 | 56.0 |
| SiC (%) ≥ | 11.5 | 14.0 | 19.0 |
| C / F.C (%) ≥ | 11.5 | 5.0 | 5.0 |
| Apparent Porosity (%) ≤ | 8.5 | 11.0 | — |
| Bulk Density (g/cm³) ≥ | 2.75 | 2.90 | — |
| Crushing Strength 110 °C × 24 h (MPa) ≥ | 40.0 | 50.0 | — |
| Adhesion MOR 110 °C × 24 h (MPa) ≥ | — | — | 1.5 |
Values are typical production averages, not guaranteed minima. A batch-specific Certificate of Analysis is issued for every shipment; third-party inspection (SGS / BV / TÜV) can be arranged on request.
| Property Reported Above | ASTM | ISO | GB/T |
|---|---|---|---|
| Chemical composition — Al₂O₃, SiO₂, Fe₂O₃, TiO₂, alkali oxides | ASTM C573 | ISO 12677 | GB/T 6900 |
| Carbon / SiC content (carbon-bearing grades) | ASTM C571 | — | GB/T 17732 |
| Apparent porosity and bulk density | ASTM C20 | ISO 5017 | GB/T 2997 |
| Cold crushing strength | ASTM C133 | ISO 10059-1 | GB/T 5072 |
| Cold modulus of rupture | ASTM C133 | ISO 5014 | GB/T 3001 |
Every value in the tables above is determined by the method stated in this reference table, and the method is identified on the batch Certificate of Analysis. Where a property is not covered by a directly corresponding ISO method, the ASTM or GB/T method is applied as the reference method and stated accordingly. Third-party verification (SGS / BV / TÜV) can be arranged on request.
About XZK ASC Brick (Al₂O₃-SiC-C)
ASC brick — Al₂O₃-SiC-C — is the standard working lining material for torpedo cars and hot metal ladles, and it is a good illustration of why single-mechanism materials fail in multi-mechanism service.
Three Attacks at Once
A torpedo car lining is attacked by slag erosion, by thermal cycling on every trip, and by the chemicals used in hot metal treatment. A high-alumina brick handles the first of these and little else; it is stiff, so cycling cracks it, and it has no defence against reagent attack. ASC addresses all three by combining phases:
- Alumina — slag resistance and refractoriness.
- Silicon carbide — erosion resistance, thermal conductivity, and resistance to reagent attack.
- Carbon — non-wetting behaviour against slag and iron, plus the compliance to absorb thermal cycling.
None of these is optional in torpedo service, which is why ASC has largely displaced plain alumina in this application.
Porosity Decides Penetration
XZK-ASC-A is held to 8.5% apparent porosity — low for a carbon-containing brick. That matters because penetration, not surface wear, is what usually ends a torpedo campaign: slag and iron work in through the pore network, the hot face loses cohesion, and material comes away in chunks. Lower porosity means a slower penetration front and a longer campaign.
Grade Selection
- XZK-ASC-A — 53% Al₂O₃, 11.5% SiC, 11.5% C, porosity 8.5%, density 2.75 g/cm³. Maximum slag and penetration resistance. Metal zone and slag line where chemical attack dominates.
- XZK-ASC-B — 62% Al₂O₃, 14% SiC, 5% C, porosity 11%, density 2.90 g/cm³, CCS 50 MPa. Where erosion and mechanical duty dominate over chemical attack.
- XZK-ASC-Mortar — 56% Al₂O₃, 19% SiC, adhesion MOR ≥1.5 MPa, for jointing the working lining.
Don’t Forget the Throat and Mouth
The barrel gets the attention, but throat and mouth failures cause a disproportionate share of downtime because those areas take mechanical damage from cleaning and skull removal. They need dedicated wear-resistant shapes and a mouth castable rather than standard barrel brick. We supply the complete package — barrel, slag line, impact pad, throat and mouth, with mortar and castables — as one matched set with a material schedule and installation drawing.
Quality and Supply
Minimum order 10 metric tons for standard shapes (7–14 days) and 20 metric tons for car-shaped and throat shapes (20–35 days). Density, porosity, crushing strength and chemistry are tested per batch, along with adhesion strength for the mortar, and a Certificate of Analysis ships with every lot.
Where This Grade Sits in the Lining System
Silicon carbide and carbon grades are selected for what they do with heat rather than for what they resist. Thermal conductivity decides whether the cooling system ever sees the load, and the bonding system decides how long the material survives alkali attack and oxidation once it does.
XZK supplies asc brick (al₂o₃-sic-c) as one zone of a zoned package rather than as a standalone item: the grades normally zoned alongside it — among them casthouse asc castable — are documented on the silicon carbide and carbon refractories page, and the vessel-level architecture — where each zone starts and ends, and which mechanism actually limits the campaign — is set out on the casthouse and torpedo car page.
Campaign data measured on this class of lining — including the wear profile that drove grade selection — is published in the Severstal 600 t torpedo car fleet programme project reference.
ASC Brick (Al₂O₃-SiC-C) — Production & Application Scenarios
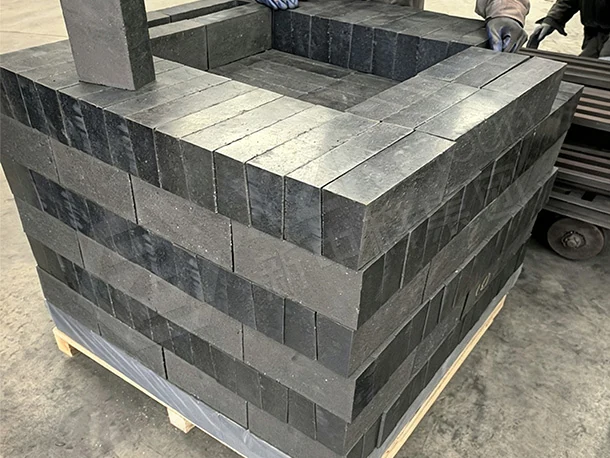
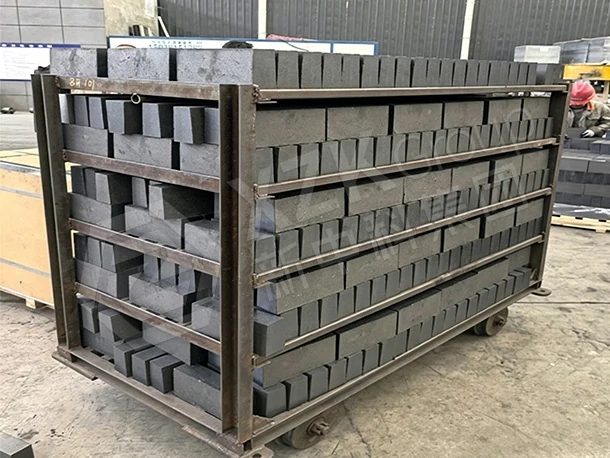
Premium raw materials, CNC pressing, high-temp firing, and on-site installation.
Advantages of Choosing XZK ASC Brick (Al₂O₃-SiC-C)
Three Mechanisms in One Material
Alumina provides slag resistance, silicon carbide adds erosion resistance and thermal conductivity, and carbon makes the body non-wetting to slag and metal. A high-alumina brick offers only the first of these.
Very Low Apparent Porosity
Held to 8.5% on XZK-ASC-A, which limits slag and iron ingress — the main reason torpedo linings lose their hot face between campaigns.
Survives Thermal Cycling
Torpedo cars cycle every trip. The carbon phase gives the compliance needed to absorb that cycling without spalling, which is where stiffer oxide materials fail.
Handles Desulfurisation Reagents
Hot metal treatment with magnesium and lime reagents is chemically aggressive. ASC bodies resist that attack far better than plain alumina or fireclay.
Specific Applications of ASC Brick (Al₂O₃-SiC-C)
Proven performance across diverse heavy industrial thermal equipment.
Torpedo Car Barrel & Metal Zone
Working lining in the barrel and metal-line areas, exposed to iron, slag and reagent attack.
Torpedo Car Slag Line & Impact Pad
The most heavily attacked zones, where low porosity and SiC erosion resistance matter most.
Torpedo Throat & Mouth
Throat and mouth areas subject to mechanical cleaning, thermal cycling and skull removal damage.
Hot Metal Ladles & Mixers
Working linings in hot metal transfer and treatment vessels with similar duty.
400+ Furnaces Trust XZK Refractory Solutions
Over 75% of our international steel and kiln clients continue multi-year long-term procurement partnerships.
Torpedo campaign went up and, just as importantly, the wear profile became even instead of developing a deep slag-line notch.
They supplied the bricks, the mortar and the throat castable as one package, which removed the compatibility guesswork.
Porosity at 8.5% was the number that sold us, and the COA confirmed it on every batch.
Mechanical cleaning at the throat used to be our weak point. The ASC shapes are holding up much better.
Frequently Asked Engineering Questions
Click any question to expand; only one answer is shown at a time.
Why not just use high-alumina brick in a torpedo car?
Because three different mechanisms are attacking the lining simultaneously: slag erosion, thermal cycling every trip, and chemical attack from desulfurisation reagents. High-alumina brick addresses slag resistance only. ASC adds silicon carbide for erosion resistance and carbon for non-wetting behaviour and thermal compliance.
What is the difference between XZK-ASC-A and XZK-ASC-B?
ASC-A carries more carbon (11.5%) and lower porosity (8.5%) for maximum slag and penetration resistance. ASC-B carries more alumina and SiC (62% / 14%) with higher density (2.90 g/cm³) and crushing strength (50 MPa) where erosion and mechanical duty dominate.
Do you supply the mortar and castables as well?
Yes. We supply matching ASC mortar (adhesion MOR ≥1.5 MPa), high-alumina castables, mouth castables and repair mixes so that the whole car lining is chemically and thermally compatible.
How do you handle the throat and mouth?
Those areas take mechanical damage from cleaning and skull removal, so they are normally lined with a dedicated mouth castable and wear-resistant shapes rather than standard barrel brick. We will specify the combination from your car drawing.
What is the MOQ and lead time?
10 metric tons for standard shapes in 7–14 days; 20 metric tons for car-shaped bricks and throat shapes in 20–35 days including tooling.
What test data is supplied?
Bulk density and apparent porosity per ASTM C830, crushing strength per ASTM C133, chemical analysis per GB/T 6900 and GB/T 16555, and adhesion strength for the mortar. Batch COA ships with every lot.
Can you supply a complete torpedo car lining package?
Yes — barrel, slag line, impact pad, throat and mouth, with mortar and castables, as a matched set with a material schedule and installation drawing.
How is it packed?
Palletised at 1.0–1.2 metric tons on ISPM-15 fumigated pallets with PE wrap, edge protectors and moisture-barrier liner.
Related Refractories & Lining Materials
Explore complementary refractory brick grades and monolithic materials for your furnace relining.
Get Your ASC Brick (Al₂O₃-SiC-C) Quote within 12 Hours
Please specify your refractory requirements by referring to the following aspects:
- ✓ Target Application: Furnace type, lining position (slag line, hearth, roof)
- ✓ Technical Specs: Operating temperature, slag chemistry, chemistry requirements
- ✓ Quantity & Dimensions: Tonnage requirement, standard or custom CAD drawing
- ✓ Delivery Terms: FOB Qingdao/Tianjin, CIF destination port
Why Steel Plants Choose XZK Refractories
Zonal Engineering, Not Just Bricks
Every proposal is a zone-by-zone material schedule matched to your furnace profile and operating practice — so all zones reach end-of-life together.
Source Factory Consistency
Fully automatic CNC batching and zero-defect quality control keep batch-to-batch variation at laboratory level.
Proven Global References
Supplied to Baosteel, Shougang, Hyundai Steel, JSW, Severstal, MMK and 400+ furnace projects across 60+ countries.
Full-Lifecycle Service
Lining design, masonry supervision, heat-up curves and failure analysis — plus EPC turnkey delivery for new builds and relines.
Send Us Your Furnace Drawing
Our engineers will return a zonal lining proposal with material schedule and quotation within 48 hours — even for non-standard shapes.
- Free material feasibility review
- Zonal architecture & installation drawings
- Heat-up curve & masonry guidance
Strict ISO 9001 Process Control Across All 6 Workshops
Every batch of raw materials is chemically assayed. Finished refractory shapes undergo density, ultrasonic non-destructive testing, and pre-assembly gap verification prior to global packaging.
- Raw material ICP chemical assay on every incoming batch
- Density, porosity and cold crushing (CCS) tests per ASTM / ISO
- Ultrasonic non-destructive testing of finished shapes
- Pre-assembly gap verification before seaworthy packaging