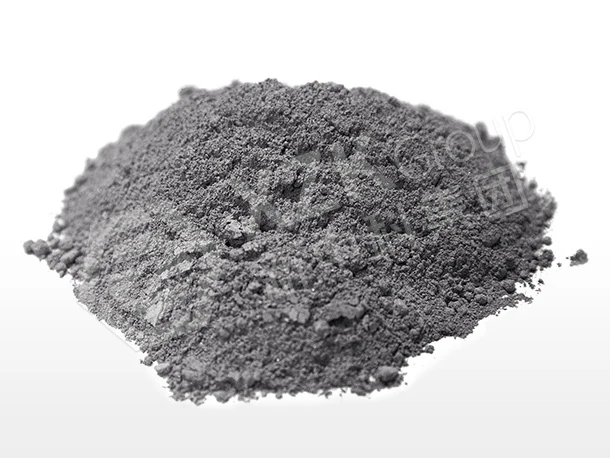
High-Conductivity Carbon Ramming Mass for Blast Furnace Hearth
C + SiC ≥90–91% · Thermal conductivity ≥10–12 W/(m·K) at 200 °C · Crushing strength ≥6–10 MPa at 1200 °C — the heat path to the coolers.
Specifications of XZK High-Conductivity Carbon Ramming Mass
Manufactured strictly in accordance with ASTM, ISO, and YB/T metallurgical refractory standards.
| Property | XZK-CG301C (BFD-S10) | XZK-CG301D (BFD-S9) |
|---|---|---|
| C + SiC (%) ≥ | 91.0 | 90.0 |
| Moulded Bulk Density (g/cm³) ≥ | 1.9 | 1.9 |
| Crushing Strength (1200 °C × 3 h, MPa) ≥ | 10.0 | 6.0 |
| Thermal Conductivity (200 °C, W/m·K) ≥ | 12.0 | 10.0 |
Values are typical production averages, not guaranteed minima. A batch-specific Certificate of Analysis is issued for every shipment; third-party inspection (SGS / BV / TÜV) can be arranged on request.
| Property Reported Above | ASTM | ISO | GB/T |
|---|---|---|---|
| Chemical composition — Al₂O₃, SiO₂, Fe₂O₃, TiO₂, alkali oxides | ASTM C573 | ISO 12677 | GB/T 6900 |
| Carbon / SiC content (carbon-bearing grades) | ASTM C571 | — | GB/T 17732 |
| Apparent porosity and bulk density | ASTM C20 | ISO 5017 | GB/T 2997 |
| Cold crushing strength | ASTM C133 | ISO 10059-1 | GB/T 5072 |
| Thermal conductivity | ASTM C201 | ISO 8894-1 | GB/T 5990 |
Every value in the tables above is determined by the method stated in this reference table, and the method is identified on the batch Certificate of Analysis. Where a property is not covered by a directly corresponding ISO method, the ASTM or GB/T method is applied as the reference method and stated accordingly. Third-party verification (SGS / BV / TÜV) can be arranged on request.
About XZK High-Conductivity Carbon Ramming Mass
High-conductivity carbon ramming mass is the last link in a chain, and a chain is only as good as its weakest link. Heat leaves a blast furnace hearth by travelling from the lining, through the carbon block, through the ramming layer, and into the cooling element. If that layer is poorly conductive or badly compacted, the whole path is compromised.
The Layer Nobody Specifies Properly
Specifying excellent carbon brick and then treating the ramming layer as a commodity filler is a common and expensive mistake. The layer has two jobs — conduct heat, and fill completely — and both depend on the material and on how it is installed.
XZK-CG301C carries thermal conductivity ≥12 W/(m·K) at 200 °C with C+SiC ≥91% and crushing strength ≥10 MPa at 1200 °C. XZK-CG301D runs at ≥10 W/(m·K) and ≥6 MPa. Choose on the thermal duty and the mechanical requirement at that position.
Compaction Determines Conductivity
The rated conductivity assumes the specified installed density. Under-compacted ramming mass contains voids, and voids are insulation — so the thermal path degrades exactly where it needs to perform. This is why we ask about ramming access and gap width before quoting, and why we specify layer thickness and compaction method with the material. A crew that gets compaction right is worth more than a marginally better product.
Specified as Part of the Hearth, Not Separately
We specify the ramming mass together with the microporous carbon, the ceramic cup and the stack, bosh and belly grades, so the whole hearth build-up is thermally consistent. Assembling a hearth from parts chosen independently is how mismatches occur — and a mismatch in thermal conductivity is invisible until the furnace is running and temperatures start climbing.
Supply
Minimum order 5 metric tons, shipped in 7–14 days, with grading adjusted for your ramming access and gap width. Batch test data covering C+SiC content, moulded bulk density, crushing strength at 1200 °C and thermal conductivity ships with every lot, along with a written installation procedure.
Where This Grade Sits in the Lining System
Monolithic materials fail more often on installation than on specification. Water demand, mixing time, vibration and the first heat-up curve decide the outcome before the lining ever sees metal — which is why installation parameters are issued with the material instead of being left to site practice.
XZK supplies high-conductivity carbon ramming mass as one zone of a zoned package rather than as a standalone item: the grades normally zoned alongside it — among them microporous carbon brick — are documented on the monolithic refractories page, and the vessel-level architecture — where each zone starts and ends, and which mechanism actually limits the campaign — is set out on the blast furnace page.
Campaign data measured on this class of lining — including the wear profile that drove grade selection — is published in the MMK Magnitogorsk No.10 BF and 375 t ladle programme project reference.
High-Conductivity Carbon Ramming Mass — Production & Application Scenarios
Premium raw materials, CNC pressing, high-temp firing, and on-site installation.
Advantages of Choosing XZK High-Conductivity Carbon Ramming Mass
Closes the Thermal Gap
The ramming layer sits between the carbon block and the cooling element. If it has poor conductivity or is poorly compacted, the entire hearth cooling path is compromised — regardless of how good the carbon brick is.
Compaction Is the Whole Job
Thermal conductivity of a ramming mass depends heavily on installed density. We grade for your ramming access and gap width and specify layer thickness and compaction so the material reaches its rated conductivity.
Adequate Crushing Strength
Crushing strength of 6–10 MPa at 1200 °C gives the layer dimensional stability under the hearth load without becoming rigid and cracking.
Matched to the Carbon Build-Up
Specified together with our microporous carbon and ceramic cup so the whole hearth build-up is thermally consistent rather than assembled from parts with mismatched properties.
Specific Applications of High-Conductivity Carbon Ramming Mass
Proven performance across diverse heavy industrial thermal equipment.
Blast Furnace Hearth
The ramming layer between hearth carbon blocks and the cooling staves or shell.
Hearth Bottom
Under-hearth ramming layers above the bottom cooling.
Sidewall & Cooler Gaps
Gap filling between carbon sidewall blocks and cooling elements.
400+ Furnaces Trust XZK Refractory Solutions
Over 75% of our international steel and kiln clients continue multi-year long-term procurement partnerships.
Hearth temperatures came down and stabilised once the ramming layer was properly specified and compacted. It was the missing link.
They asked about our ramming access and gap width before quoting, which told us they understood the job.
Thermal conductivity was verified on the batch and matched the stated figure.
Layer thickness and compaction instructions were specific enough that our crew got it right first time.
Frequently Asked Engineering Questions
Click any question to expand; only one answer is shown at a time.
Why does this layer matter so much?
Because it is the last link in the hearth cooling chain. Heat travels from the lining through the carbon block, through the ramming layer, into the cooler. If that layer is poorly conductive or badly compacted, the chain is broken and hearth temperatures rise — no matter how good the carbon brick is.
CG301C or CG301D?
CG301C has higher thermal conductivity (≥12 W/(m·K)) and higher crushing strength (≥10 MPa); CG301D runs at ≥10 W/(m·K) and ≥6 MPa. Choose on the thermal duty and the mechanical requirement at that position.
How important is compaction?
Critical. The rated conductivity assumes the specified installed density. Under-compacted ramming mass leaves voids that act as insulation, and the thermal path degrades. We specify layer thickness and compaction method with the material.
Can it be used for gap filling at coolers?
Yes — it is commonly used to fill gaps between carbon sidewall blocks and cooling elements, where both conductivity and complete filling matter.
What is the MOQ and lead time?
5 metric tons, shipped in 7–14 days, with grading adjusted for your ramming access and gap width.
What documentation is provided?
Batch test data covering C+SiC content, moulded bulk density, crushing strength at 1200 °C and thermal conductivity, plus a written installation procedure with layer thickness and compaction guidance.
Is it part of a complete hearth package?
Yes. We specify it together with microporous carbon, ceramic cup and the stack, bosh and belly grades so the whole build-up is thermally consistent.
How is it packed?
25 kg moisture-barrier bags on ISPM-15 pallets, date-stamped, with 1,000 kg big bags available.
Related Refractories & Lining Materials
Explore complementary refractory brick grades and monolithic materials for your furnace relining.
Get Your High-Conductivity Carbon Ramming Mass Quote within 12 Hours
Please specify your refractory requirements by referring to the following aspects:
- ✓ Target Application: Furnace type, lining position (slag line, hearth, roof)
- ✓ Technical Specs: Operating temperature, slag chemistry, chemistry requirements
- ✓ Quantity & Dimensions: Tonnage requirement, standard or custom CAD drawing
- ✓ Delivery Terms: FOB Qingdao/Tianjin, CIF destination port
Why Steel Plants Choose XZK Refractories
Zonal Engineering, Not Just Bricks
Every proposal is a zone-by-zone material schedule matched to your furnace profile and operating practice — so all zones reach end-of-life together.
Source Factory Consistency
Fully automatic CNC batching and zero-defect quality control keep batch-to-batch variation at laboratory level.
Proven Global References
Supplied to Baosteel, Shougang, Hyundai Steel, JSW, Severstal, MMK and 400+ furnace projects across 60+ countries.
Full-Lifecycle Service
Lining design, masonry supervision, heat-up curves and failure analysis — plus EPC turnkey delivery for new builds and relines.
Send Us Your Furnace Drawing
Our engineers will return a zonal lining proposal with material schedule and quotation within 48 hours — even for non-standard shapes.
- Free material feasibility review
- Zonal architecture & installation drawings
- Heat-up curve & masonry guidance
Strict ISO 9001 Process Control Across All 6 Workshops
Every batch of raw materials is chemically assayed. Finished refractory shapes undergo density, ultrasonic non-destructive testing, and pre-assembly gap verification prior to global packaging.
- Raw material ICP chemical assay on every incoming batch
- Density, porosity and cold crushing (CCS) tests per ASTM / ISO
- Ultrasonic non-destructive testing of finished shapes
- Pre-assembly gap verification before seaworthy packaging