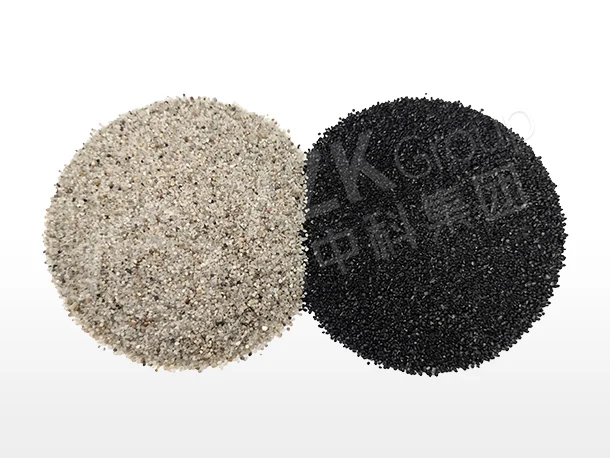
Ladle Filler Sand for High Free-Opening Rates
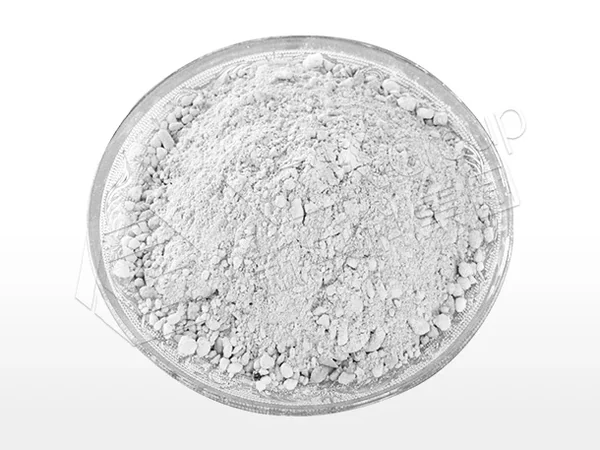
Refractory base with controlled grain size · Free-opening rate to specification · Low bulk-density increase at temperature · Consistent flow through the nozzle.
Specifications of XZK Ladle Filler Sand
Manufactured strictly in accordance with ASTM, ISO, and YB/T metallurgical refractory standards.
| Property | Typical Value |
|---|---|
| Base material | Refractory sand, graded |
| Refractoriness (°C) ≥ | 1750 |
| Bulk Density (g/cm³) | 1.6 – 2.0 |
| Grain size | Graded to nozzle bore and steel head |
| Moisture (%) ≤ | Controlled, low |
Values are typical production averages, not guaranteed minima. A batch-specific Certificate of Analysis is issued for every shipment; third-party inspection (SGS / BV / TÜV) can be arranged on request.
| Property Reported Above | ASTM | ISO | GB/T |
|---|---|---|---|
| Chemical composition — Al₂O₃, SiO₂, Fe₂O₃, TiO₂, alkali oxides | ASTM C573 | ISO 12677 | GB/T 6900 |
| Apparent porosity and bulk density | ASTM C20 | ISO 5017 | GB/T 2997 |
| Refractoriness (pyrometric cone equivalent) | ASTM C24 | ISO 528 | GB/T 7322 |
Every value in the tables above is determined by the method stated in this reference table, and the method is identified on the batch Certificate of Analysis. Where a property is not covered by a directly corresponding ISO method, the ASTM or GB/T method is applied as the reference method and stated accordingly. Third-party verification (SGS / BV / TÜV) can be arranged on request.
About XZK Ladle Filler Sand
Ladle filler sand costs very little and protects against one of the most disruptive events in a casting plant: a ladle that will not open on its own. The measure that matters is not price per ton, it is free-opening rate — and that is a function of grading and sintering behaviour.
How Free Opening Works
The sand column sits in the upper nozzle and well block above the closing plate. When the plate opens, the column should fall out under its own weight and the steel head above it, letting steel flow. For that to happen the sand must sinter enough at the top to stop steel penetrating down into the bore, but not so much that it forms a solid plug.
That balance is the entire specification. Too little sintering and steel enters the bore and freezes; too much and the ladle does not open without lancing.
Grading Is the Lever
Grain size is matched to nozzle bore and to the steel head above it. An undersized grain bridges and will not flow out; an oversized one lets steel penetrate too far before sintering takes effect. We grade against three figures — nozzle bore, steel head, and tap-to-cast time — because all three change the answer.
Moisture is the other controlled variable. Moisture causes splashing on tap and contributes hydrogen pickup, which is a steel quality issue on sensitive grades. Content is controlled and kept low on every batch.
What a Stuck Ladle Actually Costs
The sand is cheap. A ladle that does not open costs caster time, oxygen lancing, and — most importantly — puts people in front of an open ladle valve doing manual intervention. On a safety basis alone, the free-opening rate deserves more attention than it usually gets.
Supply
Minimum order 5 metric tons, shipped in 7–14 days, with grading adjusted to your nozzle bore and steel head. Batch test data covering refractoriness, bulk density, moisture and grain size distribution ships with every lot, along with a written filling procedure. If your free-opening rate is below target, send us your current rate and operating figures — often the fix is grading, not a different product.
Where This Grade Sits in the Lining System
Monolithic materials fail more often on installation than on specification. Water demand, mixing time, vibration and the first heat-up curve decide the outcome before the lining ever sees metal — which is why installation parameters are issued with the material instead of being left to site practice.
XZK supplies ladle filler sand as one zone of a zoned package rather than as a standalone item: the grades normally zoned alongside it — among them slide gate plate — are documented on the monolithic refractories page, and the vessel-level architecture — where each zone starts and ends, and which mechanism actually limits the campaign — is set out on the steel ladle and RH/VD page.
For a complete vessel programme built on this class of material, including the wear survey that set the zoning, see the JFE Steel RH degasser snorkel and ladle flow control programme project reference.
Ladle Filler Sand — Production & Application Scenarios
Premium raw materials, CNC pressing, high-temp firing, and on-site installation.
Advantages of Choosing XZK Ladle Filler Sand
Free Opening Is the Whole Point
A ladle that does not open on its own costs far more than the sand ever will — in caster disruption, in oxygen lancing, and in the safety exposure of manual intervention. Grading for free-opening rate is the specification that matters.
Sintering Behaviour Controlled
The sand must sinter enough at the top to block steel ingress but not so much that it forms a plug. That balance is a function of grain grading and refractory base, and it is what we control.
Low, Controlled Moisture
Moisture in filler sand causes splashing and, worse, hydrogen pickup. Content is controlled and kept low on every batch.
Graded to Your Nozzle
Grain size is matched to nozzle bore and the steel head above it, because an undersized grain bridges and an oversized one does not flow.
Specific Applications of Ladle Filler Sand
Proven performance across diverse heavy industrial thermal equipment.
Steel Ladle Free Opening
Filling the upper nozzle and well block before tapping to prevent steel entering the bore.
Slide Gate Systems
Used with slide gate ladles where the plate closes over the filler column.
Other Bottom-Pour Vessels
Bottom-pour and nozzle-controlled vessels requiring reliable free opening.
400+ Furnaces Trust XZK Refractory Solutions
Over 75% of our international steel and kiln clients continue multi-year long-term procurement partnerships.
Free-opening rate went up measurably after we changed to a properly graded sand. Caster disruption from stuck ladles became rare.
Consistent moisture and grain size across shipments, which is what we need for a repeatable result.
They asked about our nozzle bore and steel head before recommending a grade. That is the right question.
Filling procedure was supplied and our crew follows it. Result has been consistent.
Frequently Asked Engineering Questions
Click any question to expand; only one answer is shown at a time.
What causes a ladle to fail to open?
Usually sintering. If the sand sinters too heavily at the top of the column, it forms a plug the steel head cannot push through. The countermeasures are correct grain grading for your nozzle bore and steel head, and a refractory base with the right sintering behaviour. Moisture and fines content also play a part.
How do you grade the sand?
By nozzle bore, steel head above the nozzle, and the tapping-to-casting time. An undersized grain bridges and will not flow; an oversized one lets steel penetrate too far before it sinters. Give us those three figures and we will grade accordingly.
Why is moisture control important?
Moisture causes splashing when steel arrives and contributes hydrogen pickup, which is a steel quality issue on sensitive grades. Content is controlled and kept low on every batch.
What is the MOQ and lead time?
5 metric tons, shipped in 7–14 days, with grain grading adjusted to your nozzle bore and steel head.
What documentation is provided?
Batch test data covering refractoriness, bulk density, moisture and grain size distribution, plus a written filling procedure.
Can you help improve our free-opening rate?
Yes. Tell us your current rate, nozzle bore, steel head and tap-to-cast time, and any recent changes in practice. Often the fix is grading rather than a different product.
Is it suitable for slide gate ladles?
Yes — it is used in slide gate ladles where the plate closes over the filler column, and in stopper-controlled systems as well.
How is it packed?
25 kg moisture-barrier bags on ISPM-15 pallets, date-stamped, with 1,000 kg big bags available.
Related Refractories & Lining Materials
Explore complementary refractory brick grades and monolithic materials for your furnace relining.
Get Your Ladle Filler Sand Quote within 12 Hours
Please specify your refractory requirements by referring to the following aspects:
- ✓ Target Application: Furnace type, lining position (slag line, hearth, roof)
- ✓ Technical Specs: Operating temperature, slag chemistry, chemistry requirements
- ✓ Quantity & Dimensions: Tonnage requirement, standard or custom CAD drawing
- ✓ Delivery Terms: FOB Qingdao/Tianjin, CIF destination port
Why Steel Plants Choose XZK Refractories
Zonal Engineering, Not Just Bricks
Every proposal is a zone-by-zone material schedule matched to your furnace profile and operating practice — so all zones reach end-of-life together.
Source Factory Consistency
Fully automatic CNC batching and zero-defect quality control keep batch-to-batch variation at laboratory level.
Proven Global References
Supplied to Baosteel, Shougang, Hyundai Steel, JSW, Severstal, MMK and 400+ furnace projects across 60+ countries.
Full-Lifecycle Service
Lining design, masonry supervision, heat-up curves and failure analysis — plus EPC turnkey delivery for new builds and relines.
Send Us Your Furnace Drawing
Our engineers will return a zonal lining proposal with material schedule and quotation within 48 hours — even for non-standard shapes.
- Free material feasibility review
- Zonal architecture & installation drawings
- Heat-up curve & masonry guidance
Strict ISO 9001 Process Control Across All 6 Workshops
Every batch of raw materials is chemically assayed. Finished refractory shapes undergo density, ultrasonic non-destructive testing, and pre-assembly gap verification prior to global packaging.
- Raw material ICP chemical assay on every incoming batch
- Density, porosity and cold crushing (CCS) tests per ASTM / ISO
- Ultrasonic non-destructive testing of finished shapes
- Pre-assembly gap verification before seaworthy packaging