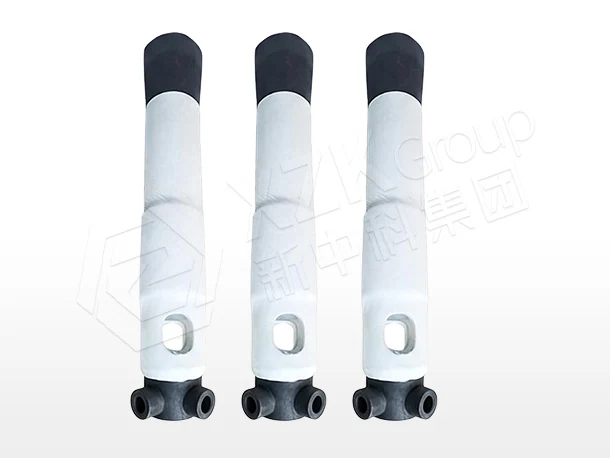
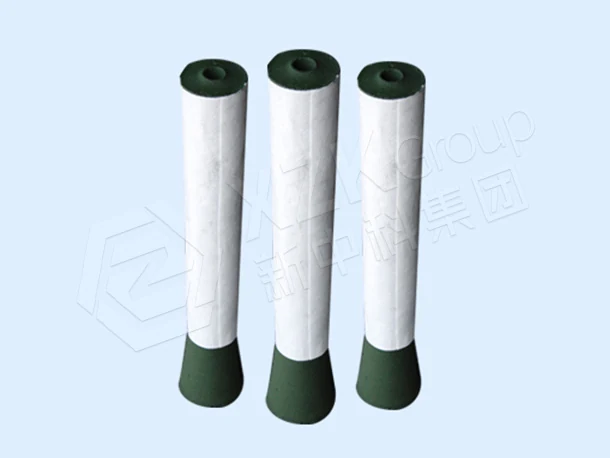
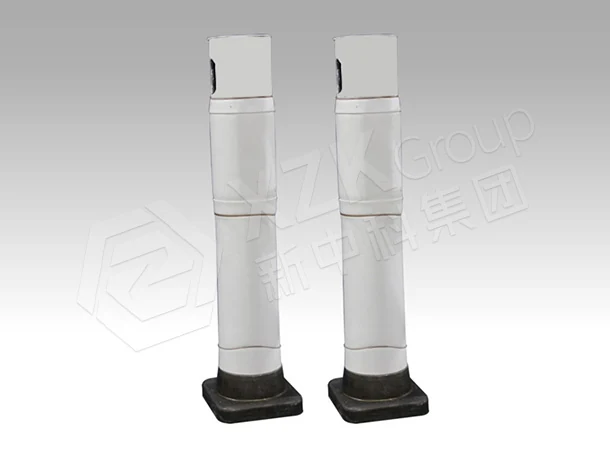
Anti-Clogging SEN — Preheat-Free, Argon-Blowing, Carbon-Free & Zirconia Grades
Body Al₂O₃ ≥40–65% · ZrO₂ 35–75% · C+SiC 8–25% · BD ≥2.10–3.50 g/cm³ · CCS ≥10–20 MPa — seven grades by steel grade.
Specifications of XZK Submerged Entry Nozzle (SEN)
Manufactured strictly in accordance with ASTM, ISO, and YB/T metallurgical refractory standards.
| Property | XZK-SEN-Preheat | XZK-SEN-NonPreheat | XZK-SEN-Argon | XZK-SEN-NonArgon | XZK-SEN-NonCarbon | XZK-SEN-Z45 | XZK-SEN-ZSP |
|---|---|---|---|---|---|---|---|
| Section | Body | Anti-clogging (Al₂O₃) | Body | ZrO₂ | Body | Slag line | Slag line |
| Al₂O₃ (%) ≥ | 40.0 | 45.0 | 43.0 | — | 65.0 | — | — |
| ZrO₂ (%) ≥ | — | — | — | 35.0 | — | 75.0 | 65.0 |
| C + SiC (%) ≥ | 25.0 | 20.0 | 20.0 | 15.0 | ≤ 8.0 | 11.0 | 15.0 |
| MgO (%) ≥ | — | — | — | — | 18.0 | — | — |
| Bulk Density (g/cm³) ≥ | 2.25 | 2.36 | 2.10 | 2.58 | 2.65 | 3.50 | 3.30 |
| Apparent Porosity (%) ≤ | 19.0 | 19.0 | 25.0 | 21.0 | 20.0 | 22.5 | 20.0 |
| Cold Crushing Strength (MPa) ≥ | 19.0 | 20.0 | 10.0 | 18.0 | 18.0 | 16.0 | 16.0 |
| Cold Modulus of Rupture (MPa) ≥ | 6.0 | 6.0 | — | — | — | 3.0 | 3.0 |
Values are typical production averages, not guaranteed minima. A batch-specific Certificate of Analysis is issued for every shipment; third-party inspection (SGS / BV / TÜV) can be arranged on request.
| Property Reported Above | ASTM | ISO | GB/T |
|---|---|---|---|
| Chemical composition — MgO, CaO, SiO₂, Fe₂O₃, Al₂O₃ | ASTM C574 | ISO 12677 | GB/T 5069 |
| Carbon / SiC content (carbon-bearing grades) | ASTM C571 | — | GB/T 17732 |
| Apparent porosity and bulk density | ASTM C20 | ISO 5017 | GB/T 2997 |
| Cold crushing strength | ASTM C133 | ISO 10059-1 | GB/T 5072 |
| Cold modulus of rupture | ASTM C133 | ISO 5014 | GB/T 3001 |
Every value in the tables above is determined by the method stated in this reference table, and the method is identified on the batch Certificate of Analysis. Where a property is not covered by a directly corresponding ISO method, the ASTM or GB/T method is applied as the reference method and stated accordingly. Third-party verification (SGS / BV / TÜV) can be arranged on request.
About XZK Submerged Entry Nozzle (SEN)
Submerged entry nozzles are where the central tension in continuous casting refractories becomes unavoidable. Erosion resistance and anti-clogging performance pull in opposite directions, and no single material is best at both. That is why XZK supplies seven SEN configurations rather than one.
The Trade You Cannot Avoid
More carbon and a denser body resist erosion — but carbon is also what drives alumina deposition inside the bore, and deposition is what causes clogging. Reduce the carbon and the bore stays cleaner, but the nozzle wears faster. Every SEN specification is a position on that curve, and the correct position depends on your steel grade and sequence length.
Four Anti-Clogging Mechanisms
- Carbon-free liner — XZK-SEN-NonCarbon: 65% Al₂O₃ with 18% MgO and C+SiC held to ≤8%. Removes the carbon that drives deposition. The usual answer for aluminium-killed and low-carbon grades.
- Argon blowing — XZK-SEN-Argon: injects gas to keep the bore clear mechanically rather than chemically.
- Zirconia liner — XZK-SEN-NonArgon (35% ZrO₂): resists slag-band attack where the band, not the bore, is the limit.
- Preheat-free — removes the preheat step and the thermal shock at start of cast.
Different symptoms need different mechanisms. If flow rate falls through a sequence, the problem is deposition — use a carbon-free liner or argon. If the nozzle fails at the slag band, use zirconia. Diagnosing which one you have is the whole job.
Zirconia Slag-Band Grades
On thin-slab and high-throughput casters, wear concentrates at the slag band in exactly the way it does on a ladle shroud, only faster. XZK-SEN-Z45 (75% ZrO₂) and XZK-SEN-ZSP (65% ZrO₂) put a zirconia band at that location, and on the right caster they pay for themselves through additional heats.
Geometry Is Not a Detail
Port angle, bore diameter and submergence depth determine the flow pattern in the mould, and that pattern governs surface quality and inclusion behaviour. A nozzle that is dimensionally correct but geometrically wrong for your mould will produce defects even though nothing has failed. We produce to drawing and confirm dimensions before production.
Supply
Quoted per set, typically 200–500 pieces minimum, 20–35 days from drawing approval. Dimensional inspection reports, batch test data and material certificates ship with every order, and third-party inspection can be arranged.
Where This Grade Sits in the Lining System
Flow-control refractories are consumed on the caster's schedule, so the specification is as much about dimensional repeatability and interchangeability with your existing mechanism as it is about composition. A plate or shroud that fits but varies by a millimetre between lots costs more in breakouts than it saves in unit price.
XZK supplies submerged entry nozzle (sen) as one zone of a zoned package rather than as a standalone item: the grades normally zoned alongside it — among them ladle shroud (long nozzle) — are documented on the continuous casting functional refractories page, and the vessel-level architecture — where each zone starts and ends, and which mechanism actually limits the campaign — is set out on the tundish flow control page.
For a complete vessel programme built on this class of material, including the wear survey that set the zoning, see the Colakoglu Metalurji slab caster flow control programme project reference.
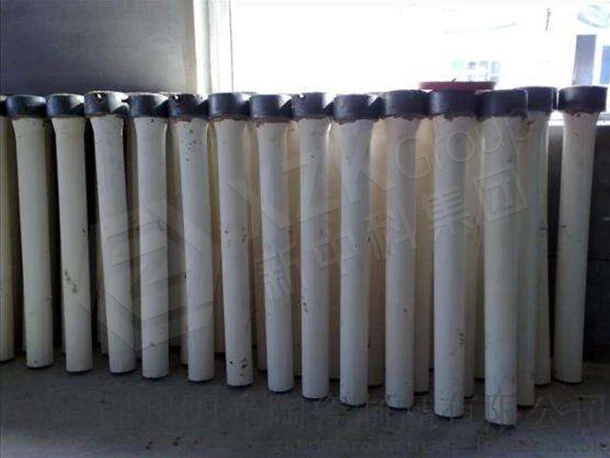
Submerged Entry Nozzle (SEN) — Production & Application Scenarios
Premium raw materials, CNC pressing, high-temp firing, and on-site installation.
Advantages of Choosing XZK Submerged Entry Nozzle (SEN)
Erosion and Clogging Pull in Opposite Directions
Higher carbon and denser bodies resist erosion but promote alumina deposition, which causes clogging. Lower carbon and carbon-free liners reduce deposition but wear faster. Seven grades let you match the liner to the steel grade rather than compromising.
Four Anti-Clogging Mechanisms
Preheat-free removes the thermal shock step; argon-blowing keeps the bore clear; carbon-free liners remove the carbon that drives deposition; zirconia liners resist slag-band attack. Different problems need different answers.
Zirconia Slag-Line Grades
XZK-SEN-Z45 (75% ZrO₂) and ZSP (65% ZrO₂) protect the slag band, which is where thin-slab and high-throughput casters usually lose the nozzle.
Geometry Made to Your Mould
Length, bore diameter, port angle and submergence depth are produced to drawing so the flow pattern in your mould is what the design intended.
Specific Applications of Submerged Entry Nozzle (SEN)
Proven performance across diverse heavy industrial thermal equipment.
Slab & Thin-Slab Casters
Continuous and thin-slab casting with long sequences, using zirconia slag-line grades.
Aluminium-Killed & Low-Carbon Grades
Carbon-free and argon-blowing designs for grades prone to clogging.
Billet & Bloom Casters
Standard and preheat-free designs for smaller-section continuous casting.
400+ Furnaces Trust XZK Refractory Solutions
Over 75% of our international steel and kiln clients continue multi-year long-term procurement partnerships.
Clogging was costing us mid-sequence interventions on aluminium-killed heats. The carbon-free liner reduced them substantially.
Zirconia slag-band grades let us run longer on the thin-slab line. That band was always the limit.
Argon blowing kept the bore clear and stabilised our flow rate through the sequence.
Port angles and submergence were exactly to drawing, so the mould flow pattern matched our model.
Frequently Asked Engineering Questions
Click any question to expand; only one answer is shown at a time.
Why are there so many SEN grades?
Because erosion resistance and anti-clogging performance are in direct tension. More carbon and higher density resist erosion but promote alumina deposition; less carbon and carbon-free liners reduce deposition but wear faster. No single grade is best, so the liner has to be matched to the steel grade and the sequence length.
Which grade for aluminium-killed steel?
Usually a carbon-free liner (XZK-SEN-NonCarbon, 65% Al₂O₃ with 18% MgO, C+SiC ≤8%) or an argon-blowing design, depending on how severe the clogging is. If you are seeing mid-sequence flow restriction, start there.
When is a zirconia slag-line grade justified?
On thin-slab and high-throughput casters, and anywhere the slag band — not the bore — is what ends the nozzle. XZK-SEN-Z45 (75% ZrO₂) and ZSP (65% ZrO₂) resist slag-band dissolution far better than an alumina-carbon body.
Do you supply preheat-free SENs?
Yes. Preheat-free designs remove the preheat step, cutting turnaround and eliminating a common source of thermal shock damage at the start of cast.
What is the MOQ and lead time?
Quoted per set, typically 200–500 pieces minimum, with 20–35 days lead time from drawing approval. New port geometries requiring tooling take longer, which we confirm with the quotation.
What documentation is provided?
Dimensional inspection reports, batch physical and chemical test data and material certificates. Third-party inspection can be arranged.
Can you match our existing SEN geometry?
Yes. Send a drawing or a sample and we will reproduce length, bore diameter, port angle and submergence depth, or propose a change based on your mould flow model.
How are SENs packed?
Individually boxed with moulded protection and palletised on ISPM-15 heat-treated pallets with moisture-barrier wrapping, with desiccant available for long sea voyages.
Related Refractories & Lining Materials
Explore complementary refractory brick grades and monolithic materials for your furnace relining.
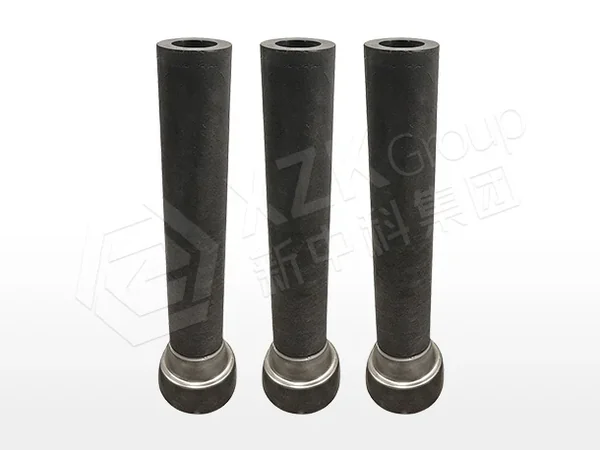
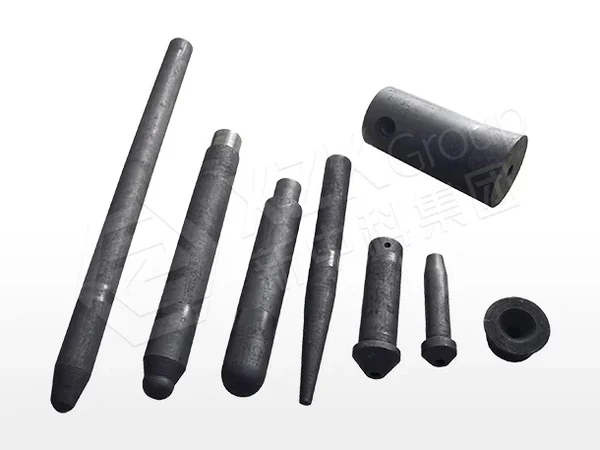
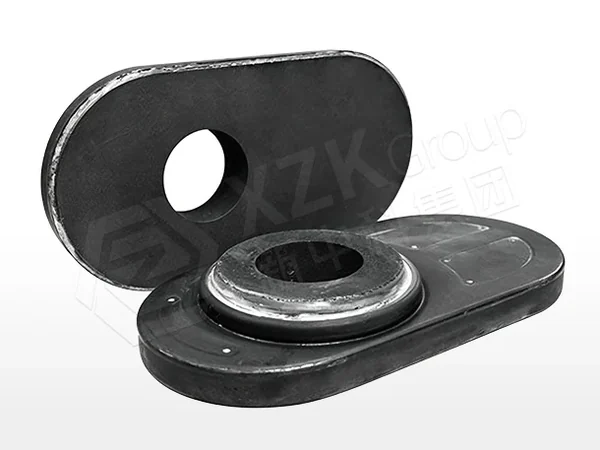
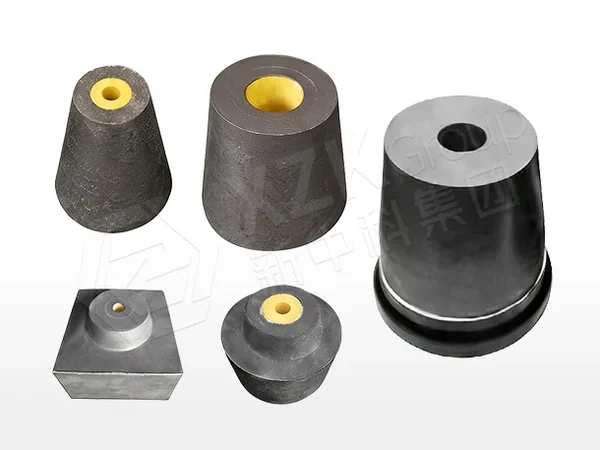
Get Your Submerged Entry Nozzle (SEN) Quote within 12 Hours
Please specify your refractory requirements by referring to the following aspects:
- ✓ Target Application: Furnace type, lining position (slag line, hearth, roof)
- ✓ Technical Specs: Operating temperature, slag chemistry, chemistry requirements
- ✓ Quantity & Dimensions: Tonnage requirement, standard or custom CAD drawing
- ✓ Delivery Terms: FOB Qingdao/Tianjin, CIF destination port
Why Steel Plants Choose XZK Refractories
Zonal Engineering, Not Just Bricks
Every proposal is a zone-by-zone material schedule matched to your furnace profile and operating practice — so all zones reach end-of-life together.
Source Factory Consistency
Fully automatic CNC batching and zero-defect quality control keep batch-to-batch variation at laboratory level.
Proven Global References
Supplied to Baosteel, Shougang, Hyundai Steel, JSW, Severstal, MMK and 400+ furnace projects across 60+ countries.
Full-Lifecycle Service
Lining design, masonry supervision, heat-up curves and failure analysis — plus EPC turnkey delivery for new builds and relines.
Send Us Your Furnace Drawing
Our engineers will return a zonal lining proposal with material schedule and quotation within 48 hours — even for non-standard shapes.
- Free material feasibility review
- Zonal architecture & installation drawings
- Heat-up curve & masonry guidance
Strict ISO 9001 Process Control Across All 6 Workshops
Every batch of raw materials is chemically assayed. Finished refractory shapes undergo density, ultrasonic non-destructive testing, and pre-assembly gap verification prior to global packaging.
- Raw material ICP chemical assay on every incoming batch
- Density, porosity and cold crushing (CCS) tests per ASTM / ISO
- Ultrasonic non-destructive testing of finished shapes
- Pre-assembly gap verification before seaworthy packaging